Capabilities
Metal Fabrication
Our fabrication hall cuts, forms and welds plate up to 25 millimetres in 316L stainless, corten weathering steel, S355 structural steel and marine-grade aluminium. Every joint is dressed back by hand after welding so the finished surface reads as one continuous form.
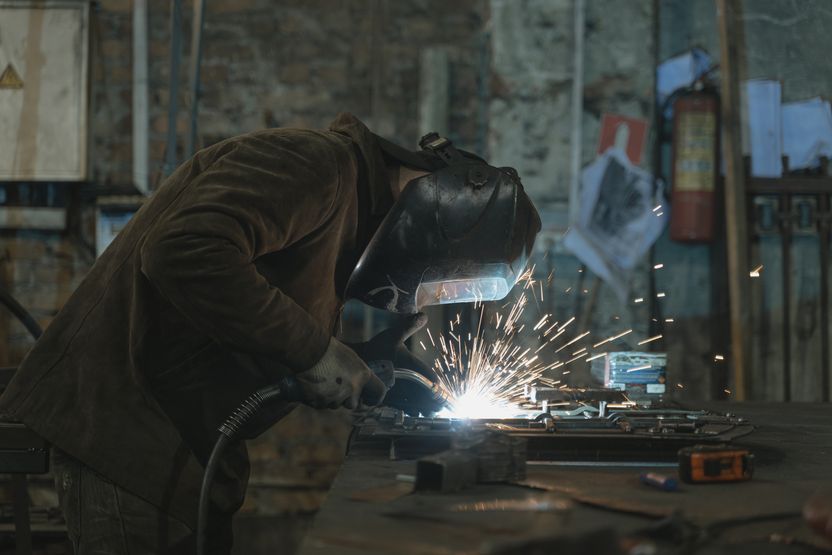
In the workshop
What we do
Plate is nested and profiled on a 6 kW fibre laser with a 3,000 by 1,500 millimetre bed, cutting 316L to 20 millimetres and mild steel to 25. Larger components are plasma profiled. Forming is done on a 400-tonne press brake and a set of plate rolls for cylindrical and conical work; complex double-curvature panels are formed over CNC-profiled ribs and finished by English wheel and hand planishing. Welding is TIG for stainless and aluminium and MIG for structural steel. Rolled ring work is produced in halves, joined on a jig and stress-relieved before finishing, which is what holds roundness to within 4 millimetres over six metres. Distortion control is planned rather than corrected: welding sequence, back-stepping and restraint are decided before the first arc is struck. All welds on visible surfaces are ground flush and blended, then the whole piece is finished after assembly so no weld shows a different grain or reflection. Dimensional verification is by laser tracker against the production model on anything over four metres, with a recorded deviation report issued at handover.
Stage by stage
How it runs
Typical durations for this stage. They are what we programme against, not best cases.
Nesting and profiling
Plate nested from the production model and cut on the fibre laser or plasma table.
Typical duration: 1 week
Forming
Press brake, plate rolls and rib-forming for double curvature; ribs cut from the same model.
Typical duration: 1–3 weeks
Assembly and welding
Jigged assembly, qualified welding procedures, planned distortion control, stress relief where required.
Typical duration: 3–6 weeks
Dressing and verification
Welds ground and blended, laser tracker check against the model, deviation report issued.
Typical duration: 1–2 weeks
Plant and codes
Equipment and standards
Named machinery, the codes we work to, and the certifications behind them.
The plant list and workshop headcounts are not published yet. Ask us and we will send the current equipment register.
In the meantime
- How this discipline runsThe stages above, with the durations we programme against.
- All capabilitiesThe other seven disciplines a commission passes through.
- Inside the factoryWhat we can say about the plant today, and what is still being confirmed.
At handover
What you receive
Drawings, calculations, files and certificates issued as part of the commission — not on request.
Fabricated assembly, welding procedure specifications and welder certificates, material test certificates, dimensional deviation report, and match-marked section drawings.
Need metal fabrication on a live project?
Send the drawing, the model or the photograph you have. We will tell you what is achievable at that scale, what it will take, and what it will cost.
We respond to every quote request within one working day